Sep 5, 2026
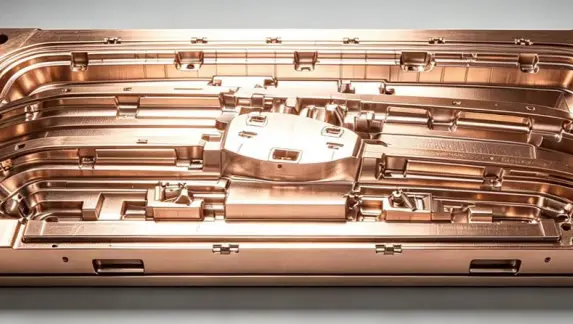
Delivery of Conformal Cooling Inserts for Automotive Injection Molds
Client: An automotive interior and exterior trim injection molding factory
Application: Front bumper injection mold (PP + 30% GF), mold weight 12 tons, annual production 300,000 units
Client's Pain Points:
The original mold was made entirely of SKD61, with an injection cycle of 65 seconds, product warpage rate of 0.3%, and 40 seconds of cooling trimming time per part. The glass fiber-filled material caused severe cavity wear, with surface scratching after 30,000 shots, and the major mold maintenance cycle was only 150,000 shots. The client had previously purchased imported beryllium copper inserts, but the delivery time was 4 weeks, the unit price exceeded the budget by 20%, and secondary processing was required for fit, making the overall cost uneconomical.
Solution:
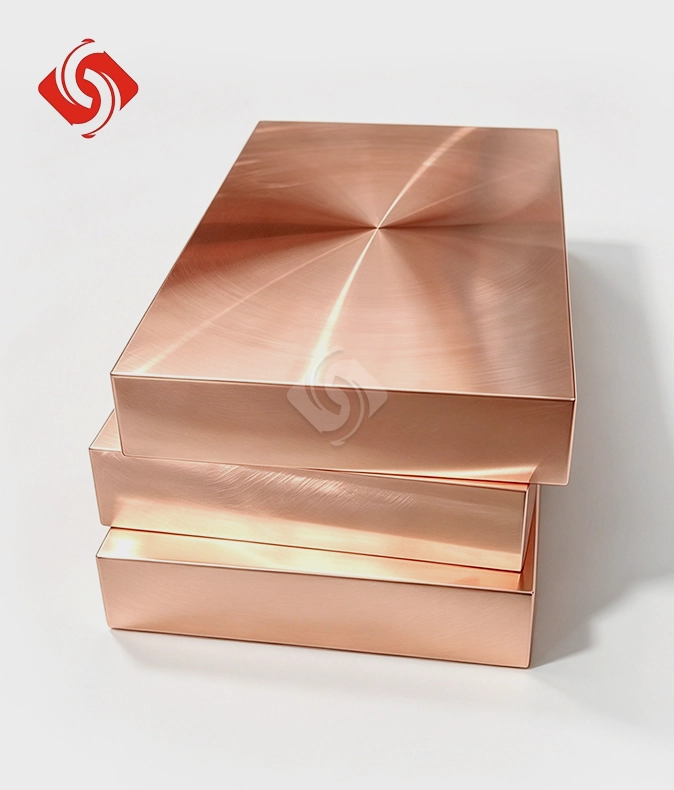
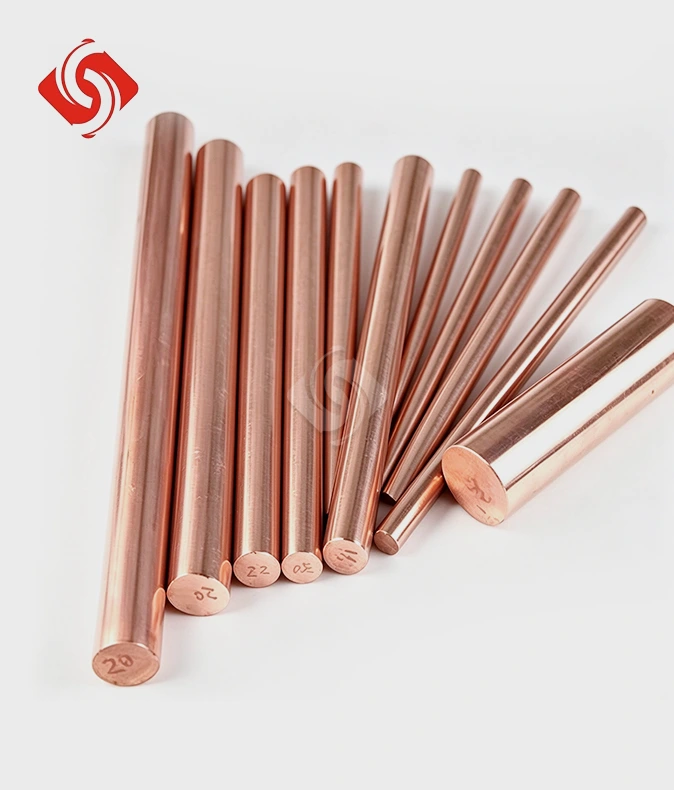
Our team provided C17200 beryllium copper plates + a one-stop CNC machining solution. We used self-produced vacuum-melted forged billets with hardness HRC 38–42 and thermal conductivity of 105 W/(m·K). Eight conformal cooling inserts were machined according to the client's drawings, with a fit clearance of ≤ 0.03mm to the mold core and nickel plating on the surface. Delivery time was 2–3 weeks (including machining + heat treatment + coating), 1–2 weeks shorter than imported alternatives, with a cost reduction of approximately 20%. Our inventory includes C17200 plates in thicknesses of 10–60mm, supporting emergency orders with 7-day delivery.
Results:
- Injection cycle reduced from 65s to 50s (23% improvement)
- Warpage rate reduced from 0.3% to 0.08%
- Trimming time per part reduced from 40s to 8s
- Insert service life reached 500,000 shots, major maintenance cycle extended by 3x