Sep 5, 2026
Mass Delivery of 800V Connector Terminals for New Energy Vehicles
Client: A Tier 1 supplier of automotive connectors
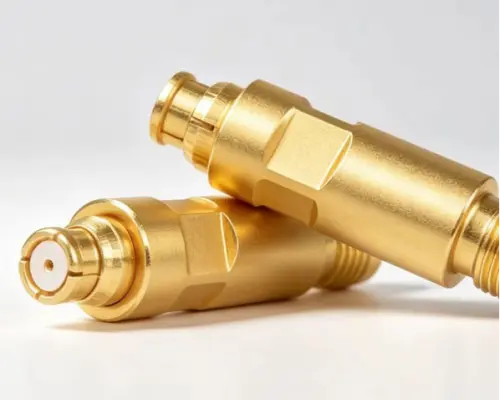
Application: Battery module connector terminals for 800V high-voltage platforms, requiring 1000+ hours of high-temperature aging testing
Client's Pain Points:
The client previously used C18150 chromium zirconium copper terminals from another brand. Under continuous high-current conditions at 125°C, the contact pressure decayed by over 20%. After high-temperature aging, the insertion force dropped from 3.2N to 2.1N, falling below the 2.5N minimum standard, resulting in batch returns.
Additionally, the client reported that C17510 sourced from other channels had unstable aging hardness, with HV fluctuations exceeding 60 within the same batch, a 15% cracking rate during bending, and blistering after nickel plating, causing production line shutdowns.
Solution:
Our company supplied C17510 beryllium nickel copper precision strips with Be content of 0.3–0.5%. The process involved vacuum melting to ensure uniform composition, large-tonnage forging to eliminate segregation, and customized two-stage aging (460°C × 2h + 480°C × 1h) to achieve peak precipitation strengthening that matched the client's bending schedule. Each batch was delivered with full inspection reports covering hardness, conductivity, and chemical composition. The initial 100kg sample was delivered within 2 weeks and moved to mass production after passing the client's PPAP verification.
Results:
- Production yield: 96% (vs. 85% with previous solution)
- Aging hardness: HV 340–360, batch-to-batch fluctuation ±10
- Insertion force retention after 1000h high-temperature aging: 88% (industry standard: 75%)
- Monthly stable delivery: 1000kg, zero returns from client
Online Message
YOU MAY LIKE