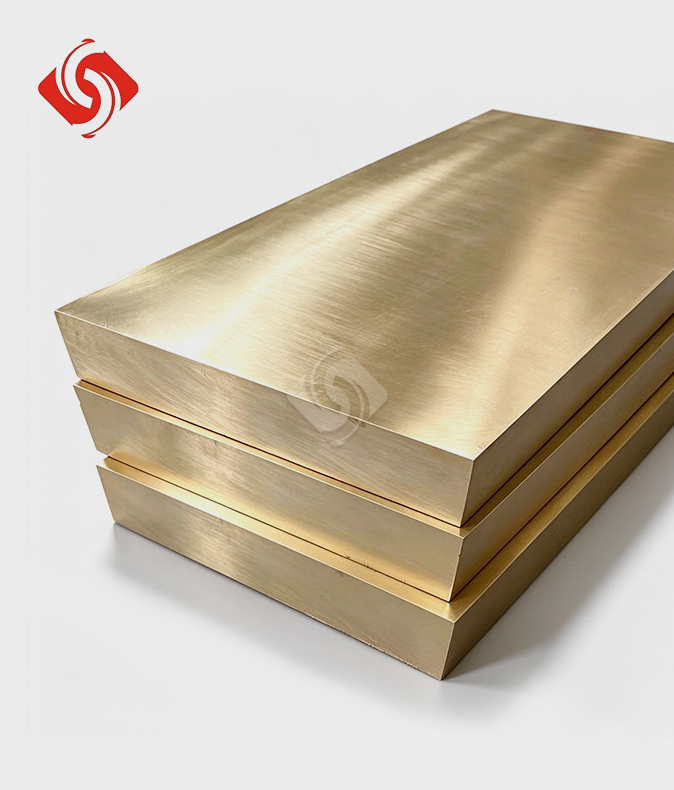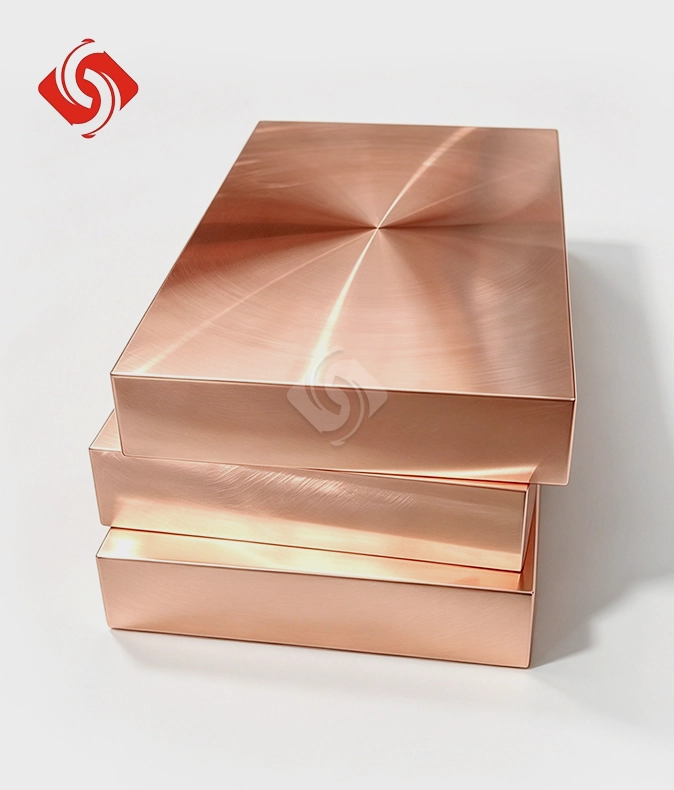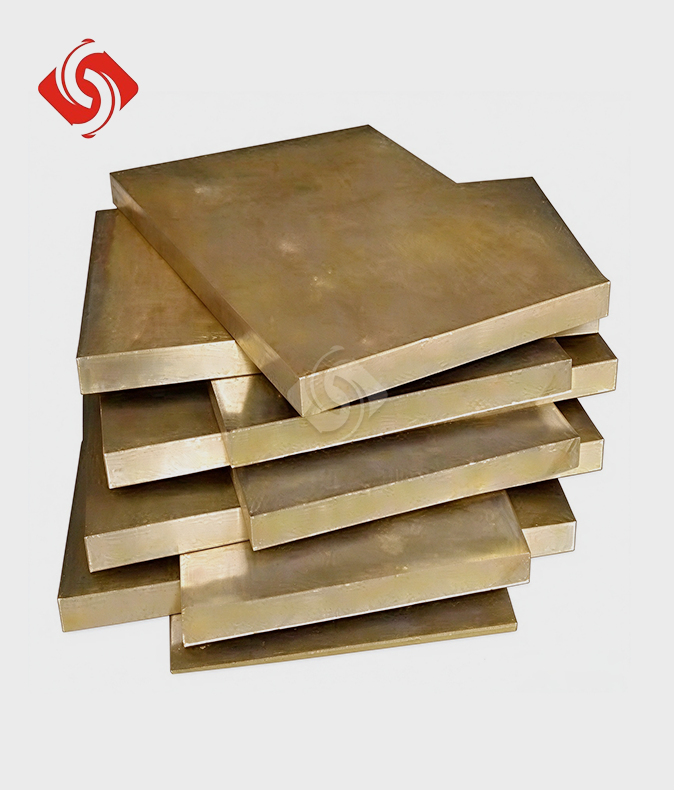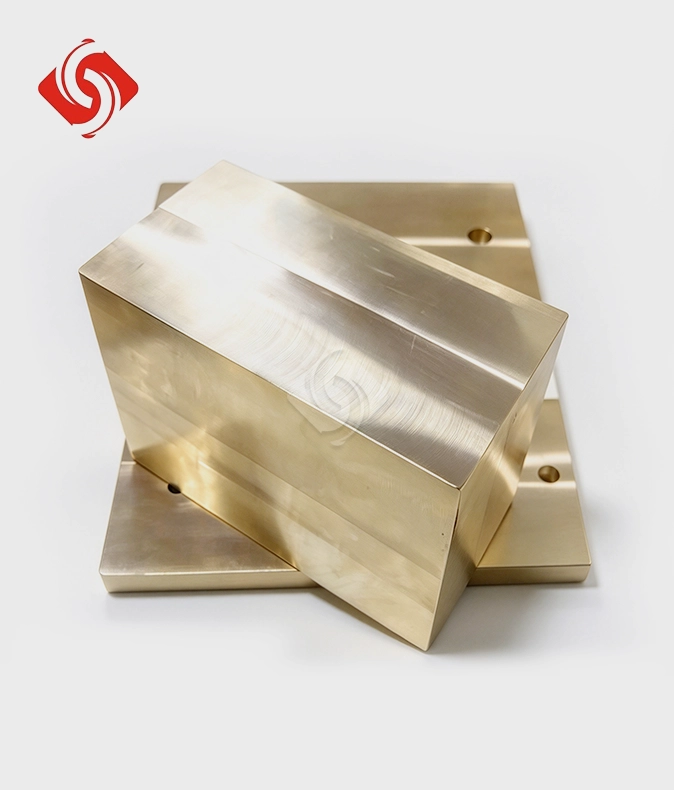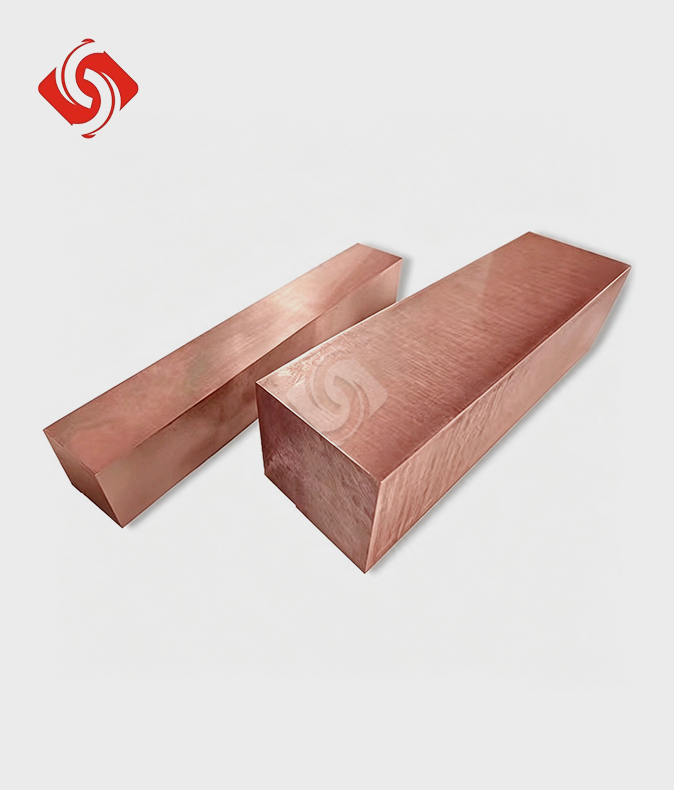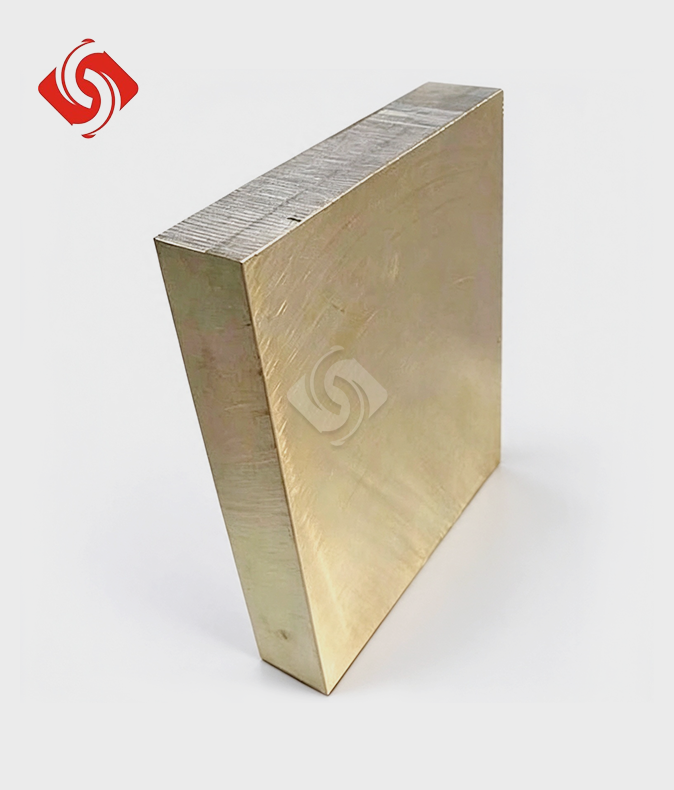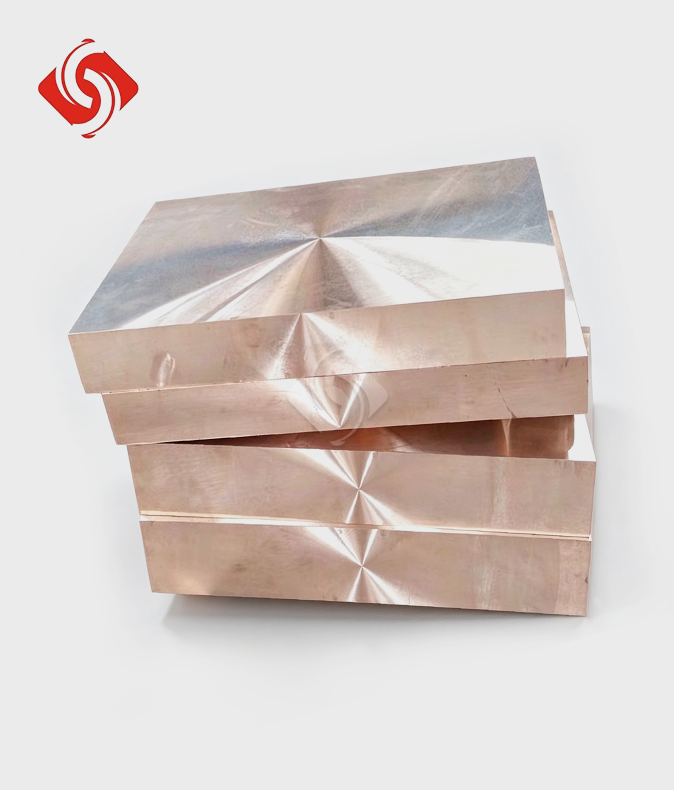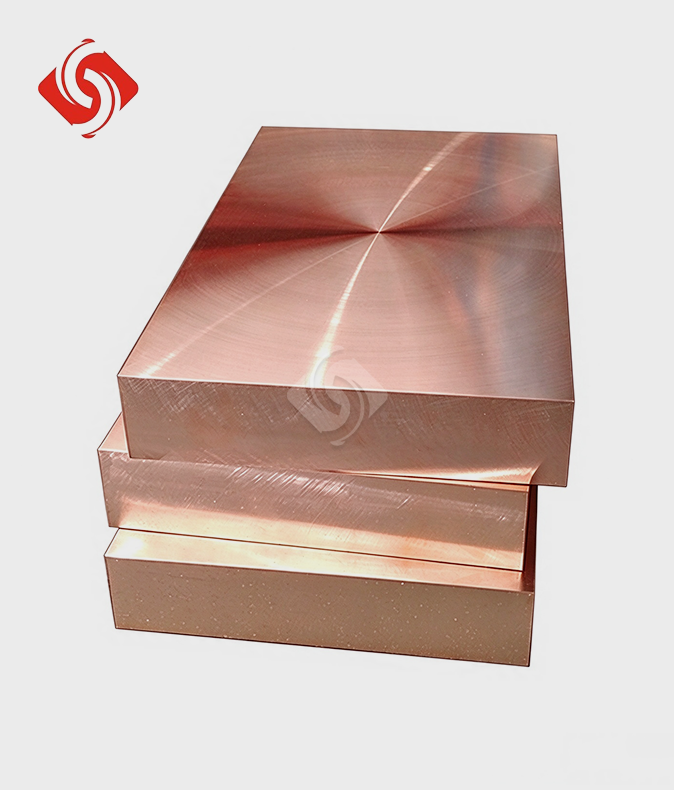
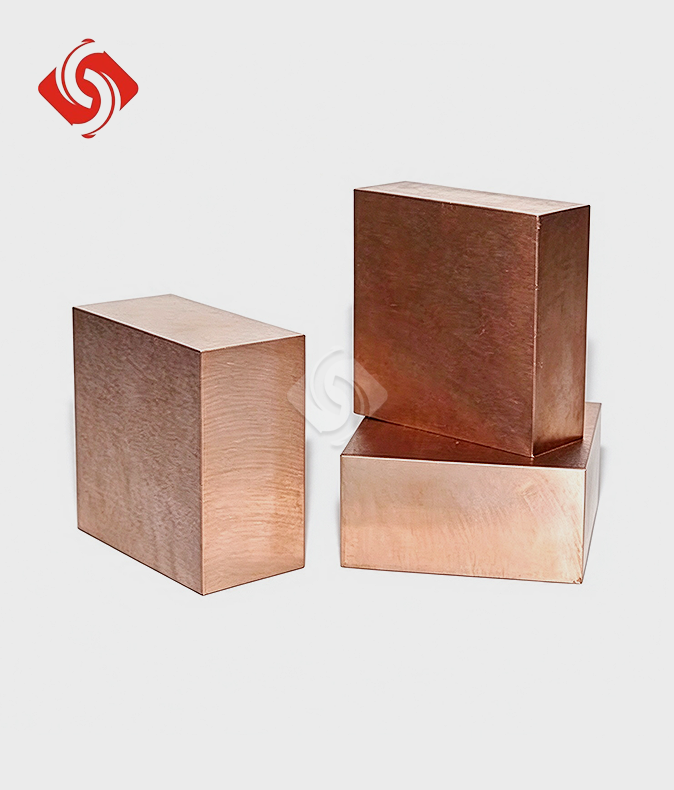
C17500 Beryllium Cobalt Copper Plate Welding
Grade Equivalents: UNS C18150 / CuCr1Zr / DIN 2.1293 / EN CW106C / RWMA Class 2
Application Focus: Resistance Welding Electrodes, Seam Welder Wheels, Current-Carrying Sheets, & Heat Sinks
Executive Standards: RWMA Class 2, ISO 5182, ASTM B702, EN 12163
Size Range: Thickness 0.5 mm – 50 mm, Width up to 1500 mm, Custom Cut-to-Size Available
Temper Condition: Solution Heat-Treated & Age-Hardened (TF00 / HT) or Cold-Rolled Tempers
Core Purpose: High Electrical Conductivity Combined with Elevated-Temperature Softening Resistance
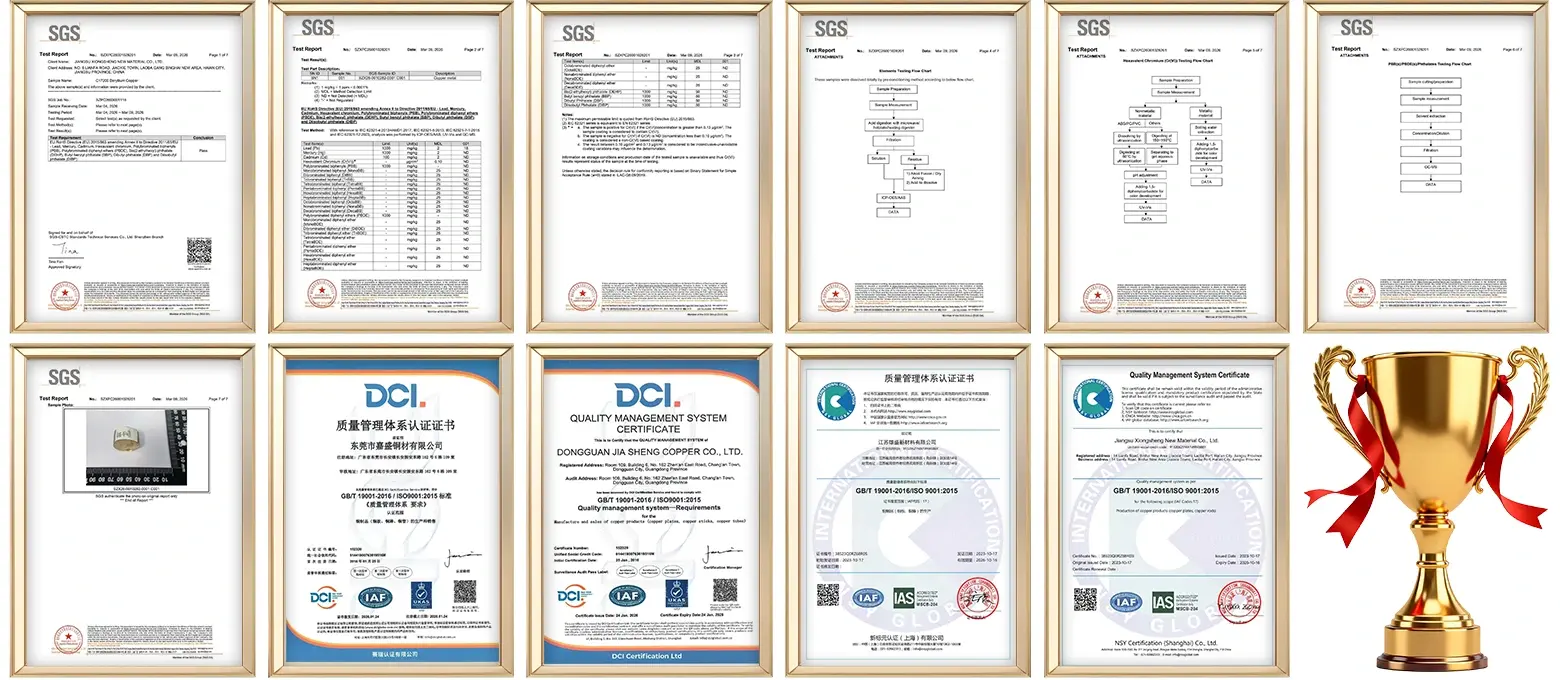
Quality Assurance: ISO 9001:2015, RoHS Compliant, EN 10204 3.1 Mill Test Certificate
Description
C17500 Beryllium Cobalt Copper Plate Welding — RWMA Class 3 Alloy for High-Conductivity Welding Applications
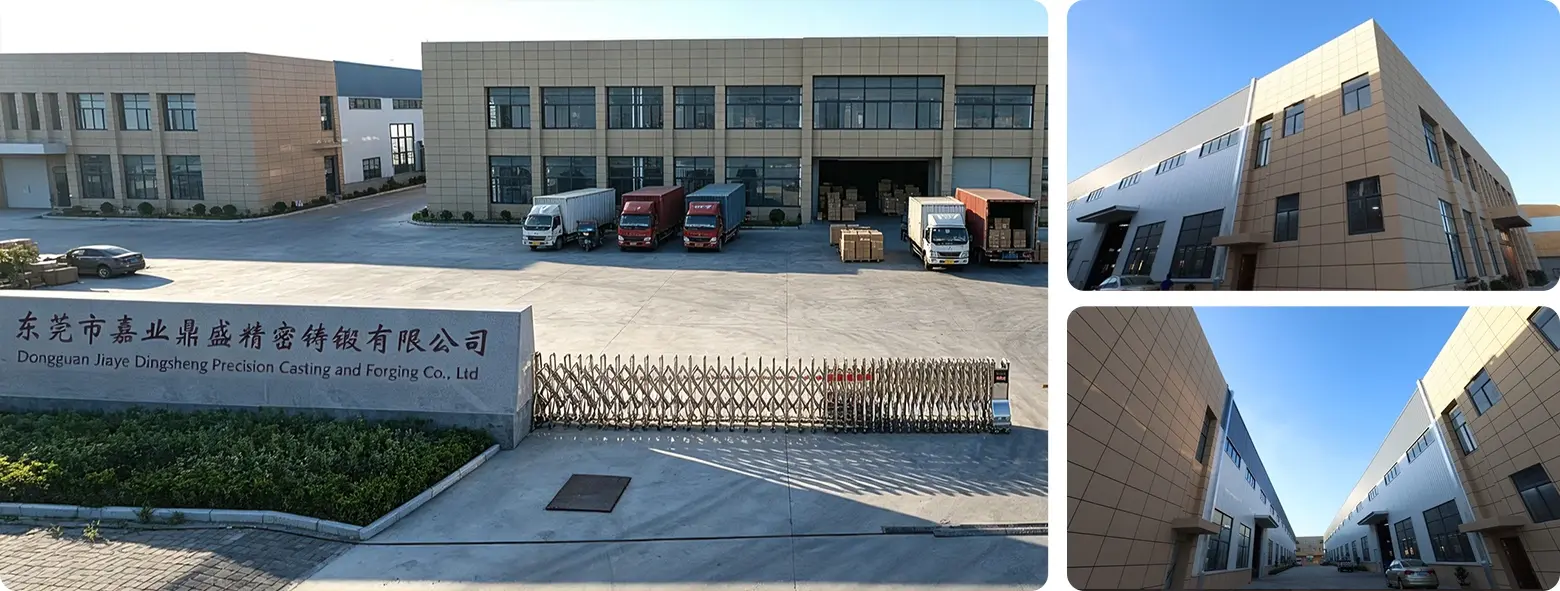
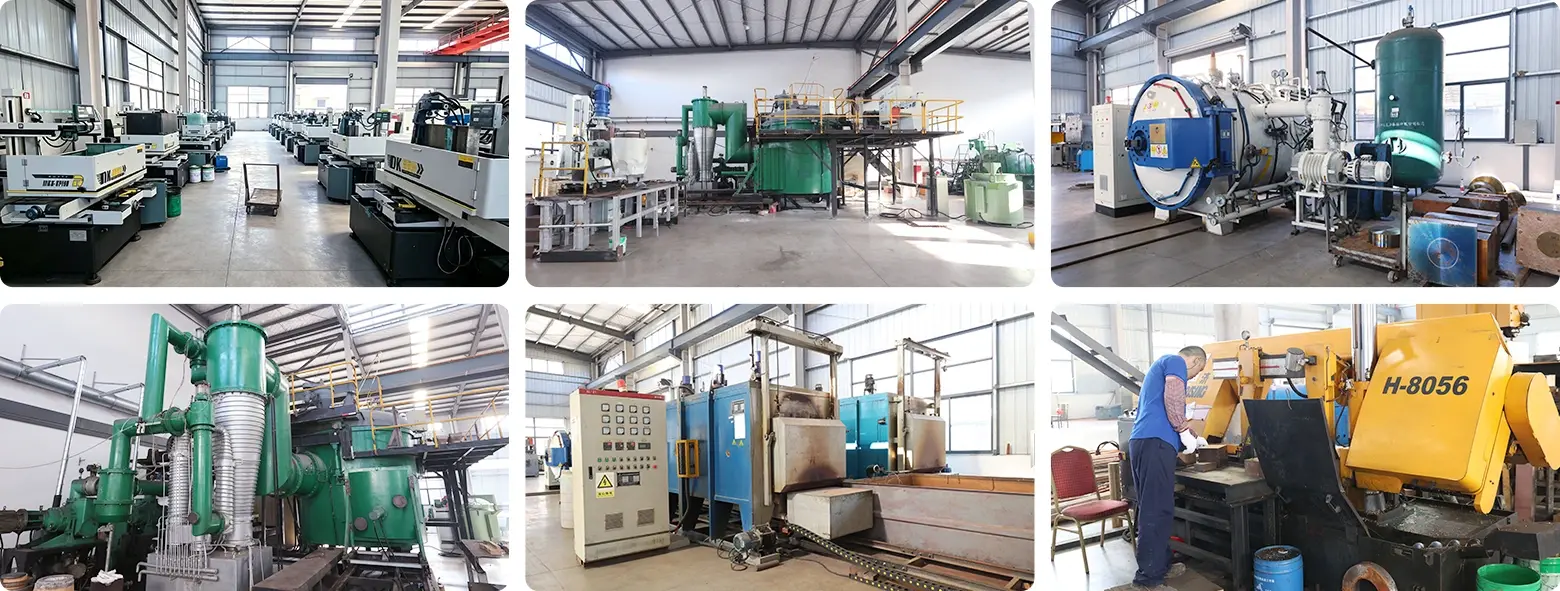
C17500 Beryllium Cobalt Copper Plate Welding uses RWMA Class 3 alloy plates, with 0.4-0.7% beryllium and 2.4-2.7% cobalt, produced according to ASTM B534 specifications. The alloy has an electrical conductivity of 45 to 60% IACS and a thermal conductivity of around 200 W/m·K. Dongguan Jiaye Dingsheng Precision Casting & Forging Co., Ltd. was founded in 1997, has more than 25 years of expertise in the manufacture of copper alloy. We do vacuum melting, precision rolling and ageing hardening in-house and provide welded plates with tensile strength over 690 MPa and hardness of 90–100 HRB following standardised post-weld heat treatment.
What Is C17500 Beryllium Cobalt Copper and Why Does Welding It Matter?
C17500 Beryllium Cobalt Copper Plate Welding For Cobalt beryllium copper alloy RWMA Class 3. When compared to the typical C17200 beryllium copper, its stable precipitation hardening structure is formed upon cooling. C17200 has increased hardness, while C17500 has improved electrical and thermal conductivity, making it perfect for parts that need reliable heat transfer and current conduction.
This alloy is to be welded with standardised process control to prevent HAZ softening. Targeted ventilation measures are necessary during operation.
C17500 Technical Specifications
| Property | Value / Range |
|---|---|
| Standard | ASTM B534 / RWMA Class 3 |
| Beryllium Content | 0.4 – 0.7% |
| Cobalt Content | 2.4 – 2.7% |
| Copper | Balance |
| Electrical Conductivity | 45 – 60% IACS |
| Thermal Conductivity | ~200 W/m·K |
| Tensile Strength (Weldment) | Min. 690 MPa |
| Hardness (Post-PWHT) | 90 – 100 HRB |
| Melting Point | ~1030 °C |
| Softening Resistance | Maintained up to elevated thermal cycling |
| Temper | Solution Heat-Treated & Age-Hardened |
| Available Forms | Plates, Bars, Strips |
Key Welding Properties and Alloy Performance
The matched cobalt and beryllium composition is favourable for continuous precipitation hardening in the welding cooling process, ensuring structural durability under welding heat. The material hardness may be maintained and recovered by post-weld ageing treatment at 450 to 480 °C. The softening of the HAZ is successfully reduced by controlling the low interpass temperature. C17500’s conductive performance is double than C17200 (20-25% IACS), which has more steady operating condition for heat dissipation and current-carrying equipment.
Welding Techniques and Process Guidelines
There are a number of mature welding procedures that are suitable for varied operating situations. Narrow HAZ with little distortion and full base metal performance is obtained via Electron Beam Welding. The TIG welding uses matching filler wire C17500 / C17510 to make the weld and base plate performance consistent. For thick plates, very regulated heat input is needed for MIG welding. In case of stainless steel welding, nickel transition layer or friction welding is advised to prevent intermetallic formations with brittle behaviour and to maintain the integrity of the joint.
Quality Control Protocols for Welded C17500 Plates
- All welded goods are fully inspected for quality.
- Eddy current testing is used to check weld conductivity.
- The quality of the interior weld is checked by ultrasonic testing.
- HAZ hardness testing indicates stable heat treatment results
- Dye penetration test removes minuscule fractures on surface.
- In the component analysis, there is no element lost in the high temperature welding.
- All batches are supplied with standard MTC test certifications and are compliant to ISO 9001 and RoHS requirements.
Industrial Applications of C17500 Welded Plates
It is extensively utilised in industrial resistance welding equipment such as automobile welding electrodes and seam wheels for resistance to pressure and heat deformation. It acts as mould cooling inserts and core pins for injection moulding, speeding up the cooling of the mould and enhancing production efficiency. It is also applicable to power electronics and new energy equipment such as high current busbars and heat sinks with stable performance in long term thermal cycling.
Why Source C17500 Welded Plates from Jiaye Dingsheng?
We adopt full in-house production procedures to avoid composition deviation from outsourcing processing. Precision rolling and calibrated heat treatment lines ensure stable dimensional tolerance and mechanical properties. We support custom size and hardness processing with free professional welding parameter guidance. In-stock goods ship within 3–5 days, and customer inquiries receive quotations within 24 hours.
Frequently Asked Questions
Q1: How to avoid hardness loss after welding?
A1: Control welding interpass temperature and conduct 450–480°C post-weld aging treatment to restore weld zone hardness.
Q2: What filler wire matches C17500 welding?
A2: C17500 or C17510 filler wire is adopted to keep consistent thermal and electrical performance.
Q3: Is there safety risk during welding?
A3: Beryllium fume requires professional ventilation and respiratory protection per industry operation standards.
Q4: Can C17500 be welded with stainless steel?
A4: Yes, nickel transition layer or friction welding is required to prevent weak welding joints.
Q5: What certification documents can be provided?
A5: EN 10204 3.1 MTC certificates with full composition, hardness and conductivity test data are supplied for each order.
Contact Us
If you have procurement and technical customization needs for C17500 Beryllium Cobalt Copper Plate Welding, please send your detailed requirements to js01@jstongcai.com.cn. Our team will provide a complete professional quotation within 24 hours.